Infrastructure pipe production places different demands on extrusion equipment depending on the polymer, dimensional requirements, and intended service conditions. PE100 pressure pipes rely on controlled melt delivery and reliable wall distribution to withstand internal pressure, while PVC drainage pipes require careful management of heat-sensitive compounds and dimensional stability.
Selecting a plastic extruder around these differences can influence production efficiency, energy consumption, and the consistency of finished pipe. Rather than comparing machines by rated output alone, manufacturers need to assess material behavior, screw geometry, operating windows, and downstream calibration as parts of one production system.
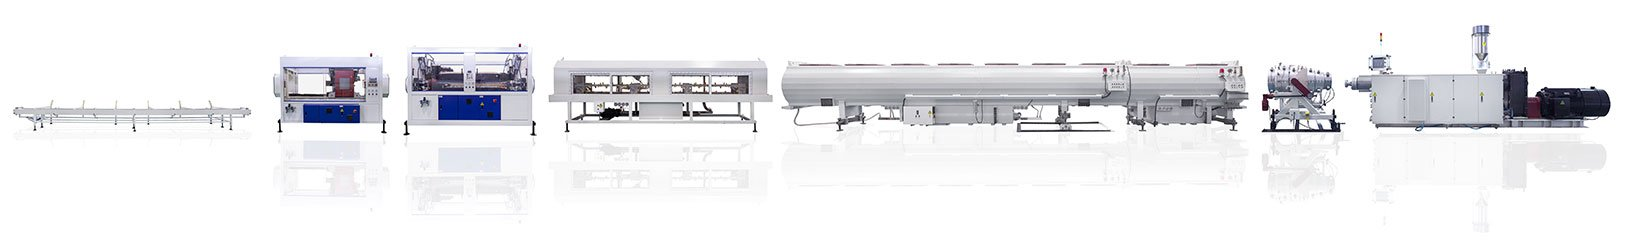
Screw Configuration and Polymer Processing Behavior
PE100 is a high-density polyethylene grade commonly used in pressurized water and gas distribution systems. Its processing characteristics make single-screw extrusion a widely used option for pipe production, particularly where stable output and consistent melt quality are required. Screw design must provide suitable melting, mixing, and conveying without creating excessive shear heating or unnecessary pressure variation. The objective is a uniform melt that can pass through the die with predictable flow around the pipe circumference.
PVC compounds present a different challenge because their thermal stability and fusion behavior require close control. Rigid PVC is commonly processed with conical or parallel twin-screw extruders, which can provide the conveying and mixing characteristics needed for formulated powders and heat-sensitive materials. Excessive residence time or localized overheating may cause degradation, discoloration, and changes in mechanical properties. A pipe extrusion machine designed for PVC must be assessed for its ability to handle the specific compound formulation, stabilizer package, and required output.
The choice between single-screw and twin-screw technology should follow the material specification rather than a universal preference for one configuration. PE100 production often prioritizes consistent high-volume melt delivery, while PVC processing places greater emphasis on controlled fusion and thermal management. Screw diameter, compression characteristics, venting requirements, and gearbox capacity also affect the useful operating range. A machine that performs well with one polymer cannot automatically be assumed to provide equivalent results with another.
L/D Ratio, Output Targets, and Melt Quality
The screw length-to-diameter ratio, commonly expressed as L/D, influences how much space is available for conveying, melting, mixing, and pressure development. Longer screws can provide additional processing length, but a higher L/D ratio does not automatically translate into better pipe quality or greater productivity. The appropriate configuration depends on the polymer, screw design, target throughput, and the degree of thermal and mechanical work needed to prepare the melt.
PE100 pipe lines may use different L/D configurations to balance output and homogenization. For example, DEKUMA’s single-screw extruder range includes 45 mm and 60 mm models with 33D configurations, while certain 60 mm versions are also available in 36D. The manufacturer’s stated HDPE/MDPE output figures vary by model and configuration, illustrating why capacity should be evaluated against the intended pipe dimensions and production conditions rather than screw diameter alone. These specifications provide a reference point, not a universal benchmark for every resin grade or pipe standard.
PVC output targets require a different calculation because compound bulk density, fusion behavior, and downstream sizing influence the practical production rate. A plastic extruder running near its maximum rated capacity may experience a narrower processing window if thermal loads or pressure requirements become difficult to manage. Useful comparisons should examine kilograms per hour alongside energy consumption per kilogram, stable operating time, scrap rate, and the quality of the finished pipe. Rated throughput without these supporting measures offers only a partial picture of productivity.
Energy Consumption and Operating Efficiency
Energy use in extrusion depends on more than the main drive motor. Barrel heating, cooling systems, vacuum calibration, haul-off equipment, cutting units, and material handling all contribute to the electricity consumed per metre of finished pipe. PE100 production can demand substantial drive power at high output, particularly when large-diameter pipes require high material throughput. Stable feeding and appropriate screw speed help avoid unnecessary fluctuations that may increase energy use or compromise dimensional control.
PVC lines have a different balance of energy demands. The extruder must provide sufficient mechanical work for compound fusion while avoiding excessive heat that could damage the material. Barrel-zone settings, screw speed, cooling capacity, and the condition of the gearbox all influence the operating balance. If the compound enters the die poorly fused, increasing downstream speed will not solve the underlying problem; if it receives excessive thermal or mechanical energy, product quality may deteriorate even when output appears satisfactory.
Comparisons between equipment should use consistent measurement conditions. Specific energy consumption, expressed in kilowatt-hours per kilogram, is more meaningful when resin formulation, pipe diameter, wall thickness, output rate, and auxiliary equipment are documented. A pipe extrusion machine with a larger motor is not necessarily less efficient, since it may operate at a higher throughput or handle a more demanding product. Energy benchmarks should be established through production trials using representative materials and stable operating conditions.
Conclusion
The distinction between PE100 pressure pipe and PVC drainage pipe begins with polymer behavior and extends through screw configuration, thermal control, output planning, and calibration. Single-screw systems are widely suited to polyethylene pipe production, whereas PVC compounds often call for twin-screw technology designed around fusion and heat sensitivity.
A well-matched plastic extruder should be judged by stable output, dimensional consistency, specific energy consumption, and the quality of the finished pipe—not by capacity figures in isolation. With experience in extrusion engineering and equipment for different polymer applications, DEKUMA offers configurations that manufacturers can evaluate against their material specifications, production targets, and infrastructure pipe requirements.
